Hygienic pumps are specially designed for use in industries that require high standards of hygiene including food and beverage, pharmaceutical, cosmetics, and biotechnology manufacturing.
They are constructed from non-toxic, non-contaminating materials and are designed to:
Prime Fluid Management supplies pumps that are EHEDG and FDA-certified, and are thoughtfully engineered for ease of maintenance and cleaning once installed.
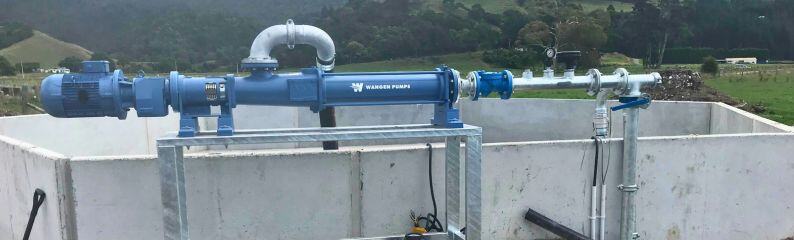
The Wangen Twin Screw combines advanced technology and service-friendly design for optimal performance and reliability:
The Hyline Series by Wangen features flexible and maintenance-free joints, and sedimentation-free design. Convey or dose food and beverages, cosmetics and pharmaceuticals.
Wangen’s KB-SL, KL-SL and KL-RF hygienic progressive cavity pumps are tailored to convey low to very high viscosity media.
Available as a mobile or stationery unit, the MX-series hygienic progressive cavity pump offers differential pressure up to 80 bar.
Wangen Twin Screw pumps ensure smooth, gentle pumping of viscous, abrasive or shear-sensitive fluids, with CIP/SIP cleaning and minimal downtime.
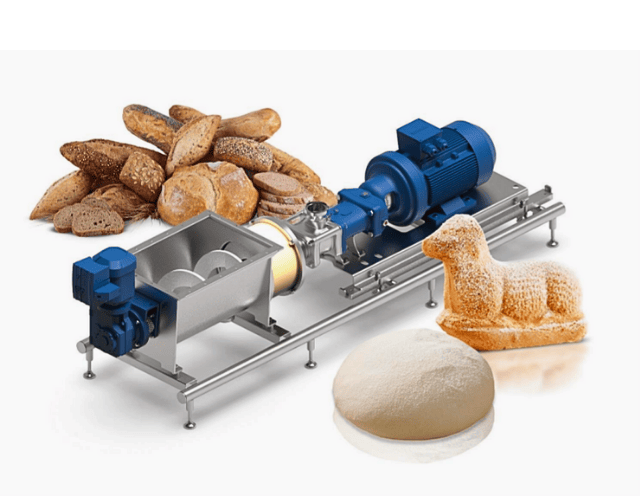
A patented feeder unit for the Wangen Twin Screw pump. Conveys highly viscous, non-flowable media with variable hopper length.
The KB-SL hygienic progressive cavities pump series offers reliability at low rotational speeds and exceptional operational safety.
The KL-SL series offers heating and cooling modes, CIP, low pulsation and superior performance over long distances and heights.
Choose hygienic double diaphragm pumps where gentle handling, self-priming and dry-running matter. SaniForce air-operated and electric pumps cover low to medium viscosity applications.
Pomac hygienic centrifugal pumps provide smooth, efficient transfer of clean, low-viscosity products – where easy cleaning is important.
Select self-priming pumps where entrained air, foam or intermittent suction disrupt centrifugal priming while hygienic CIP remains essential.
Pomac rotary lobe pumps offer gentle, reversible flow for viscous, shear-sensitive or particulate products – while preserving product integrity.
Hygienic liquid ring pumps maintain stable flow where entrained air, gas or foam disrupt conventional centrifugal pumping.
Channel impeller pumps provide efficient, gentle transfer of low to medium viscosity products containing soft solids or larger particulates.
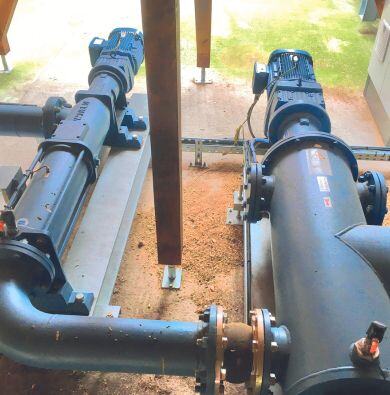
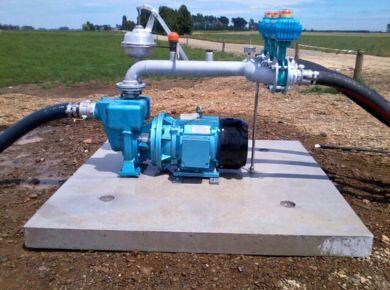
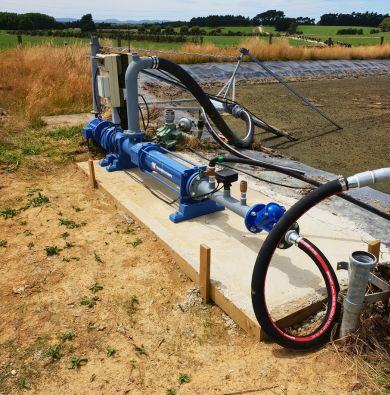
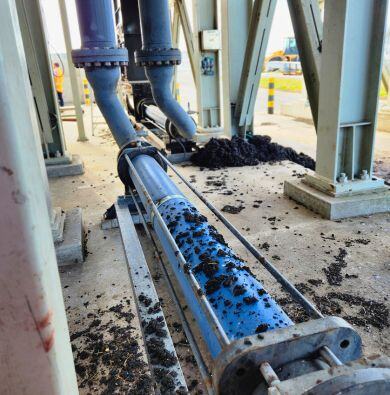
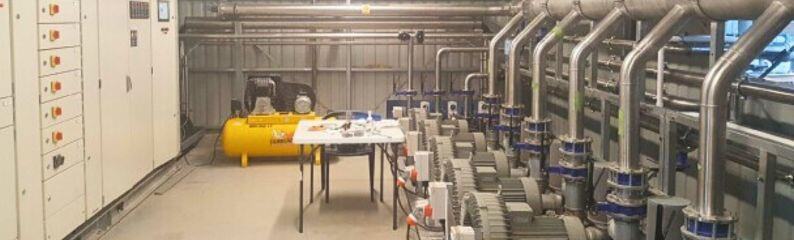
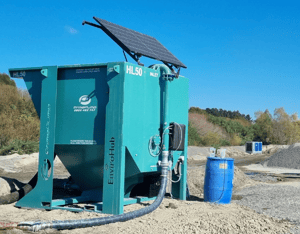
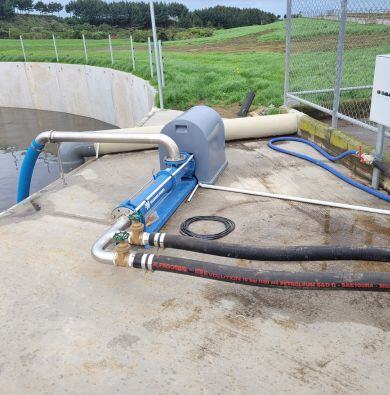
Here are some examples of our solutions being used.
At Prime Fluid Management, we understand that every fluid management challenge brings unique considerations. Here, you’ll find clear, practical answers and expert guidance to help you maximise uptime, achieve regulatory compliance, extend equipment life, and implement the most effective solution for your site.
It depends on the fluid, temperature, viscosity, and how the tank and pipework are laid out. A flooded suction setup is usually the most stable option for consistent performance, especially with higher viscosity oils, because the pump is always supplied with product.
If the pump needs to draw from a lower level or from a longer suction line, suction lift and self priming capability become important. However, the setup needs to be sized correctly to avoid issues like poor priming, air ingress, or cavitation. If you share your suction conditions and duty point, we can recommend a pump type and configuration that suits the installation.
For fuel and oil applications, reliability often comes down to protecting the pump from pressure spikes and contamination, and selecting the right sealing arrangement. Depending on the pump type and duty, options can include an internal relief or bypass valve to protect against dead heading, and an inline suction strainer to reduce the risk of damage from debris.
Seal selection also matters for demanding services, with configurations such as double mechanical seals used on certain duties where additional containment or reliability is required. We can guide you on what features make sense based on the product, operating conditions, and site requirements.
To specify the right fuel transfer pump for a New Zealand site, we typically need the fuel type, required flow rate, temperature, and viscosity, along with suction conditions such as flooded suction or suction lift.
Once we have those details, we can confirm the most suitable pump type and configuration for your application – including options for heavier fuels where viscosity is higher.