

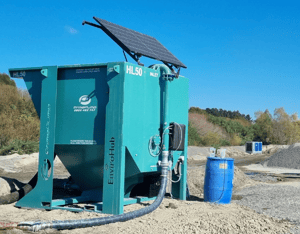
Discharge Compliance
Comprehensive water treatment and monitoring solutions
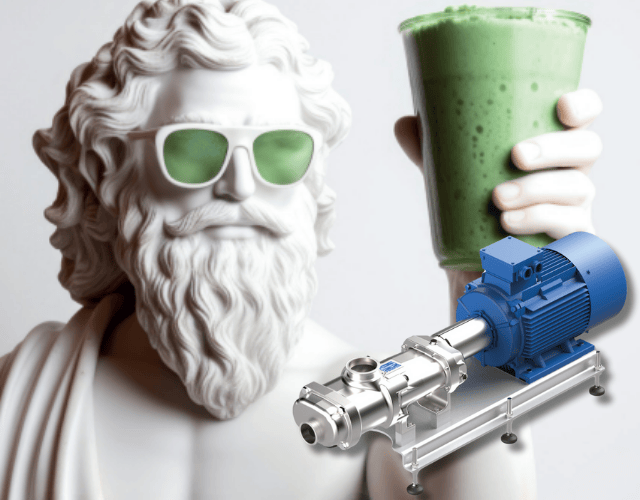
Wangen Twin Screw
Gentle handling of non-flowable media
The Wangen Twin Screw combines advanced technology and service-friendly design for optimal performance and reliability:
- Service-Friendly Design – spindle replacement without re-synchronisation/ quick seal changes.
- Wide Pressure Range – up to 30 bar.
- Gentle & Efficient – high suction lift, low pulsation, reversible pumping, wide viscosity, run dry.
- Long Service Life – enhanced shaft durability and large housing connectors for greater longevity.
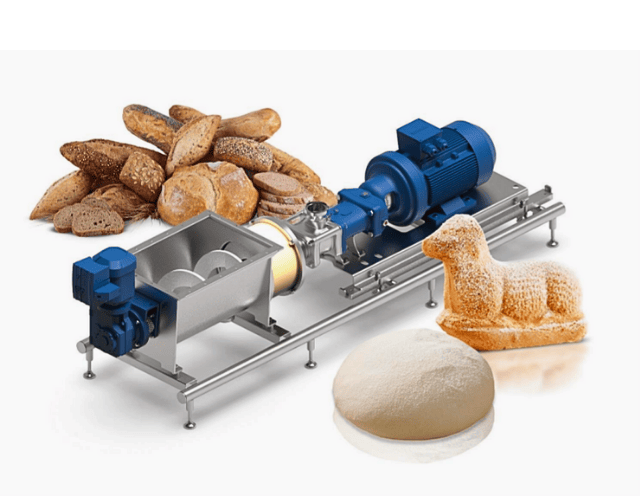
Wangen Vario Twin NG
Hopper and conveyor add-on to Wangen Twin Screw
A patented add-on to the Wangen Twin Screw pump, the Wangen Vario Twin NG with hopper and screw conveyor is designed specifically to pump highly viscous non-flowable media.- Coreless screw for ultra gentle product treatment.
- Cantilevered support of the screw results in minimal residue.
- Tailor hopper length for optimal application efficiency.
GALLERY
In the field
Here are some examples of our solutions being used.
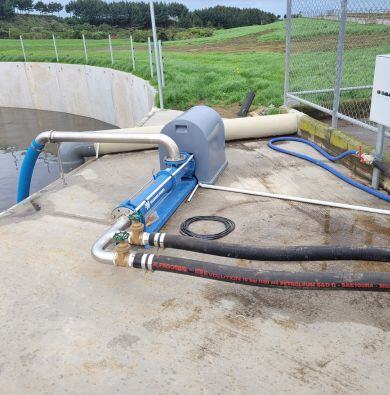
Waste water transfer
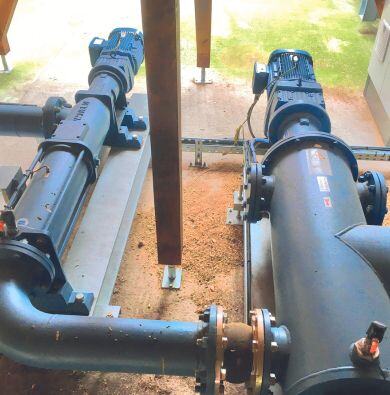
Street Photo
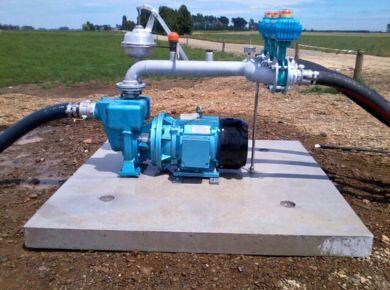
Effluent Management
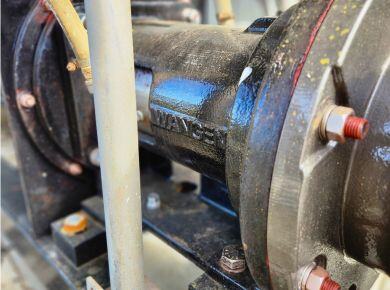
Wastewater Treament, Canterbury
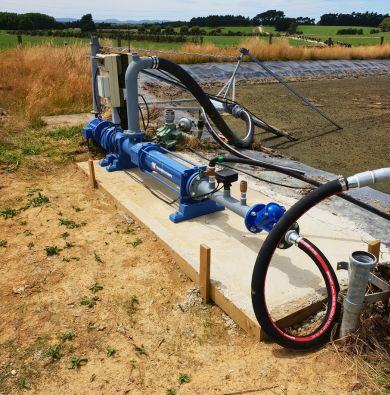
Effluent Management, Southland
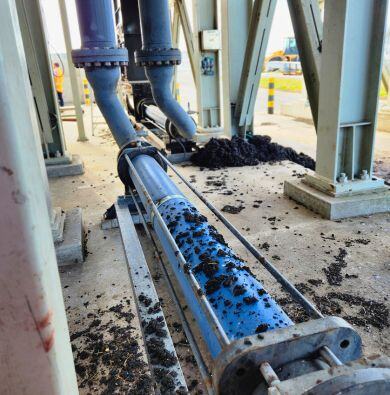
Wastewater Treatment, Canterbury
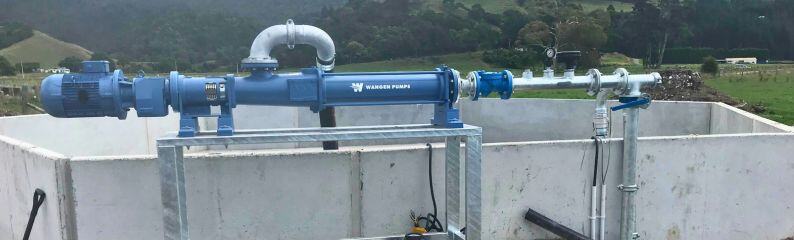
Wastewater management
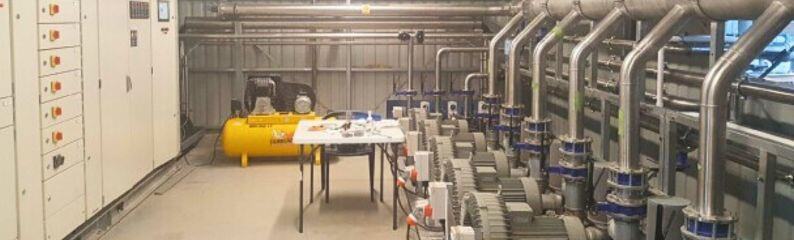
Let’s sort your fluid management needs
Speak to an expert
Tony Hylands
Industrial Pumping Solutions
Kobus van der Merwe
Industrial Sales Engineer
Charlie Petrie
Sales Manager